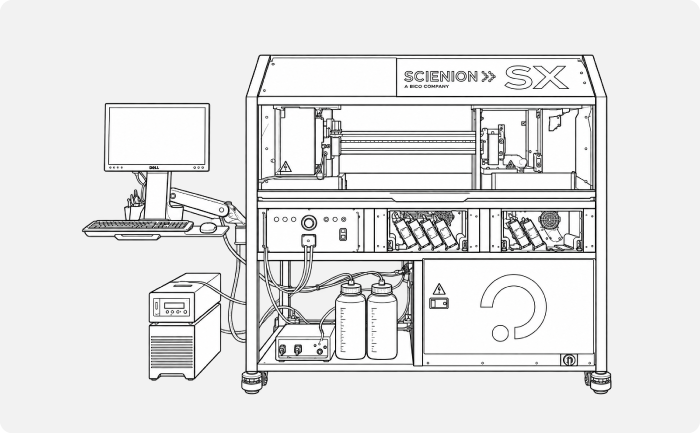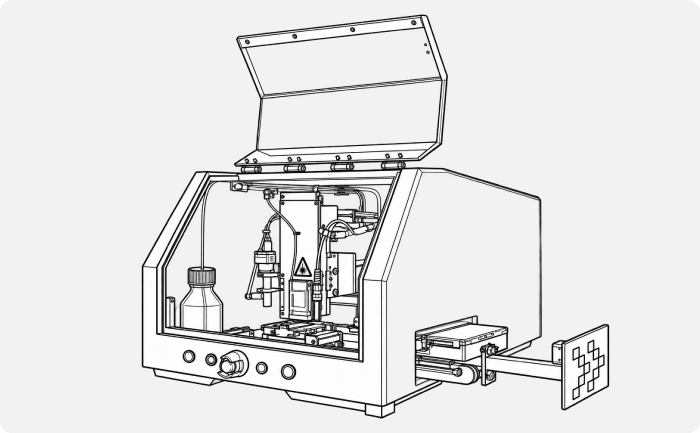


Custom fixtures, target holders, and geometries for slides, cartridges, microfluidic chips, heatable carriers, reel-to-reel modules, and multi-format plates.

Configure the number of channels, integrate dedicated reagent racks, or adopt our new conveyor-based source system allowing up to 25 reagents per run.

New instrument functions, workflows, or control logic, tailored to your process: we can implement new task sequences, user interfaces, or automated feedback loops.

Robotics, conveyors, incubators and biosafety cabinets integrated through scheduling APIs, for seamless communication with LIMS and MES systems.

Barcode and RFID tracking, QC imaging and analysis, humidity and temperature control, and inline vision for full environmental and process traceability across runs.

From application development to process optimization, our teams co-develop your process alongside the instrument, validate your assay, and prepare it for production.
Every custom project reflects the same principles that guide our technology: precision, scalability, and collaboration. Here’s what sets SCIENION and Cellenion Custom Solutions apart.


One of our big molecular diagnostics customers, manufacturing complex multi-assay IVD tests, needed to manufacture and handle more reagents in a single automated cycle without increasing footprint or setup time.
We developed the Demonstrator platform, where reagent sources move on a conveyor under stationary PDCs, and each PDC can be individually controlled and moved, enabling up to 25 reagents per run with consistent aspiration/dispense cycles.
Greater flexibility and faster batch setup. The concept proves scalable reagent multiplexing within compact systems, a prototype architecture for future high-throughput diagnostic production.
Jabil Healthcare sought to automate the deposition of diagnostic reagents inside microfluidic cartridges, ensuring picoliter accuracy, environmental stability, and complete process traceability, all within an industrial-scale cleanroom environment.
Working through our Custom Solutions process, built on communication, traceability, and quality control, our engineers designed and integrated a tailored sciFLEXARRAYER S100 line. The configuration included humidity and temperature control, reel-to-reel operation, robotic handling, RFID tracking, and inline optical QC to guarantee droplet uniformity and batch documentation.
The result was a validated and fully traceable manufacturing line capable of producing high-quality diagnostic cartridges with exceptional reproducibility and yield. It has opened the door to broaden precision medicine applications, securing Jabil’s position as a leader in diagnostics solution production.
A global biopharmaceutical automation team sought to eliminate manual steps in cell line development (CLD) while improving throughput and traceability, in an advanced bioprocess lab.
They needed to link the cellenONE HT with existing robotics, incubators, and liquid handlers to enable continuous, unattended operation for large-scale clone generation.
Our engineers adapted the cellenONE HT platform for seamless integration with external automation via Biosero Green Button Go™.
The system was configured with robotic plate handling, temperature and humidity control, and synchronized task scheduling, creating a fully walk-away workflow for automated isolation, dispensing, and tracking of single cells.
The resulting installation achieved overnight runs preparing up to 12 000 clones per cycle, delivering a 10- to 100-fold increase in throughput compared with conventional methods.
The integrated environment maintained excellent cell viability and consistent outgrowth, enabling end-to-end automation for stable cell line development.